Flux
Fluxes are the reason we can fire clay bodies and glazes in common kilns, they make glazes melt and bodies vitrify at lower temperatures.
Key phrases linking here: fluxed, flux - Learn more
Details
Fluxes are substances that promote melting in ceramic glazes and the development of glassy phases in clay bodies. More precisely, fluxing oxides interact with silica, alumina and other constituents to enable melting and vitrification at temperatures much lower than many of the individual materials could achieve on their own. Fluxes are interactors! Many are highly refractory as pure substances but become powerful melters in the presence of other oxides. Calcium oxide (CaO), for example, has a melting point of approximately 2570°C. Yet it is an important flux in stoneware glazes maturing around 1200–1300°C. The key is not the melting point of CaO itself, but its interactions with the other constituents of the glaze.
In glaze chemistry, when we discuss fluxes, we are normally referring to oxides rather than the powdered materials supplying them. The important ones include Na2O, K2O, Li2O, CaO, MgO, SrO, BaO and ZnO. B2O3 and PbO also have important fluxing roles, although their behaviour differs from that of conventional fluxing oxides.
As a glaze is heated, its raw materials undergo structural transformations, decomposition reactions, melting and dissolution. Fluxing constituents promote the formation of liquid phases and enable these to dissolve other particles. The developing melt becomes an increasingly interconnected system containing the chemical constituents of the original materials.
The effectiveness of a flux depends on the other oxides present, their proportions, temperature, atmosphere and the physical and mineralogical properties of the materials supplying them. For this reason, fluxes cannot be assigned absolute melting powers independent of the compositions in which they are used. An oxide that promotes melting in one glaze may have a much smaller effect in another. Some combinations of fluxes are especially effective because of favourable phase relationships and eutectic compositions. These interactions are often nonlinear: Relatively small changes in oxide proportions can produce surprisingly large changes in melt fluidity, crystallization and surface character.
Using multiple fluxes can be advantageous, but more is not necessarily better. The objective is to establish a combination that provides the required melting behaviour, thermal expansion, fired surface and durability.
Different fluxes for different temperatures
At low temperatures, conventional silica-alumina glazes require especially effective melting systems. Historically, PbO was widely used for this purpose, but its toxicity and potential for leaching have greatly restricted its use. Today, boron-containing frits are especially important in low- and middle-temperature glazes.
B2O3 is unusual because it functions as both a glass former and a powerful promoter of low-temperature melting. It can form glass independently, unlike most conventional fluxing oxides. In combination with alkalis, alkaline earths and other oxides, it enables glazes to mature at temperatures far below those required by traditional feldspathic compositions. It is especially valuable at low and middle temperatures.
Na2O and K2O are strong fluxes across a broad temperature range. They promote melting and can contribute to high gloss and brilliant colour development. However, they also tend to increase the thermal expansion of glazes, often making excessive amounts undesirable where crazing is a concern. Their combined contribution is commonly represented as KNaO in glaze chemistry calculations.
Li2O is another powerful flux, often effective in small amounts. It can produce substantial changes in melting behaviour, thermal expansion, colour response and crystallization. ZnO also contributes strongly to melting in suitable compositions, particularly at lower and middle temperatures. Both require careful control because changes in their proportions can have dramatic effects on the fired result. Reactive glazes commonly contain this.
CaO, MgO, SrO and BaO are especially important in stoneware glazes, although they can also participate in lower-temperature melting systems. CaO is one of the most widely used fluxing oxides. It contributes to the development of durable glasses in suitable compositions and can produce calcium-silicate crystallization and matte surfaces at higher concentrations or under appropriate cooling conditions.
MgO is especially interesting. Although refractory as a pure oxide, it can contribute to well-melted stoneware glazes while producing relatively low thermal expansion and characteristic silky matte surfaces. Adjusting the balance between MgO and higher-expansion fluxes is an important way of addressing glaze fit problems.
SrO and BaO can also produce distinctive melting, colour and crystallization effects. BaO is especially associated with certain matte and colour-development systems, although the toxicity of soluble barium compounds and the durability of barium-containing glazes require careful consideration.
Colouring oxides can also act as fluxes
Oxides normally added for colour can significantly influence melting, especially at higher concentrations. Copper, cobalt and manganese oxides are examples. Their fluxing effects depend on their oxidation states, concentrations and the chemistry of the host glaze. Iron is particularly interesting because its contribution changes with kiln atmosphere. Ferric iron (Fe₂O₃) is generally a less effective flux than ferrous iron (FeO). During reduction firing, conversion of iron toward the ferrous state can greatly increase melt fluidity. This helps explain why some iron-rich glazes melt and flow so much more in reduction than in oxidation.
Fluxing oxides are not the same as fluxing materials
The distinction between the oxide and material levels is important. Feldspar, nepheline syenite, dolomite, talc, wollastonite, calcium carbonate and frits are commonly called fluxes because they supply oxides that contribute to melting. But these materials do not necessarily melt readily by themselves. Dolomite is an excellent example. It supplies CaO and MgO to stoneware glazes, yet when calcined at very high temperatures, it becomes a refractory material suitable for demanding industrial refractory applications. Calcium carbonate likewise supplies CaO to glazes but is highly refractory by itself. Talc can promote vitrification in small additions to some clay bodies, yet high-talc compositions can be refractory.
These examples demonstrate that the fluxing action belongs to the chemical interactions occurring during firing, not simply to the melting temperature of the raw material.
Why frits can be more effective
Frits are manufactured by melting selected raw materials into a glass, cooling it and grinding it into powder. In a frit, the constituent oxides have already participated in glass formation. This can enable them to contribute to developing glaze melts more readily than when supplied by separate raw minerals.
For example, MgO supplied through an appropriately formulated frit can participate in melting earlier and more effectively than MgO supplied from talc or dolomite. The same principle can apply to other fluxing oxides. Frits also make it possible to supply combinations and proportions of oxides that are difficult to obtain using common raw materials. They can reduce gas release associated with the decomposition of carbonates, hydrates and other mineral sources.
Fluxes and glaze chemistry calculations
Glaze chemistry is especially useful for comparing the flux balances of recipes and making controlled substitutions. We can reduce one flux and increase another, compensate for changes to accompanying oxides and observe the effect on melting, thermal expansion, colour and surface character.
But predicting the absolute melting temperature of a glaze from its oxide formula remains difficult. Melting involves complex interactions, eutectics, dissolution rates, viscosity changes, crystallization and the thermal behaviour of the raw materials.
Glaze chemistry is therefore most powerful when used comparatively. Rather than expecting a formula to predict exactly how a glaze will melt, we can use it to understand why one glaze differs from another and to guide systematic adjustments. Testing then establishes whether those adjustments achieve the desired result.
Related Information
Add 5% calcium carbonate to a tenmoku. What happens?

This picture has its own page with more detail, click here to see it.
In the glaze on the left (90% Ravenscrag Slip and 10% iron oxide) the iron is saturating the melt crystallizing out during cooling. GR10-K1, on the right, is the same glaze but with 5% added calcium carbonate. This addition is enough to keep most of the iron in solution through cooling, so it contributes to the super-gloss deep tenmoku effect instead of precipitating out.
Various materials plasticized with bentonite:
Firing shrinkage varies dramatically

This picture has its own page with more detail, click here to see it.
Example of various materials mixed 75:25 with volclay 325 bentonite and fired to cone 9. Plasticities and drying shrinkages vary widely. Materials normally acting as fluxes (like dolomite, talc, calcium carbonate) are refractory here because they are fired in the absence of materials they react normally with.
Frits work much better in glaze chemistry
This picture has its own page with more detail, click here to see it.
The same glaze with MgO sourced from a frit (left) and from talc (right). The glaze is 1215U. Notice how much more the fritted one melts, even though they have the same chemistry. Frits are predictable when using glaze chemistry, it is more absolute and less relative. Mineral sources of oxides impose their own melting patterns and when one is substituted for another to supply an oxide in a glaze a different system with its own relative chemistry is entered. But when changing form one frit to another to supply an oxide or set of oxides, the melting properties stay within the same system and are predictable.
How do metal oxides compare in their degrees of melting?

This picture has its own page with more detail, click here to see it.
These metal oxides have been mixed with 50% Ferro frit 3134 and fired to cone 6 oxidation. Chrome and rutile have not melted, copper and cobalt are extremely active melters, frothing and boiling. Cobalt and copper have crystallized during cooling. Manganese has formed an iridescent glass.
At 1550F Gerstley Borate suddenly shrinks!

This picture has its own page with more detail, click here to see it.
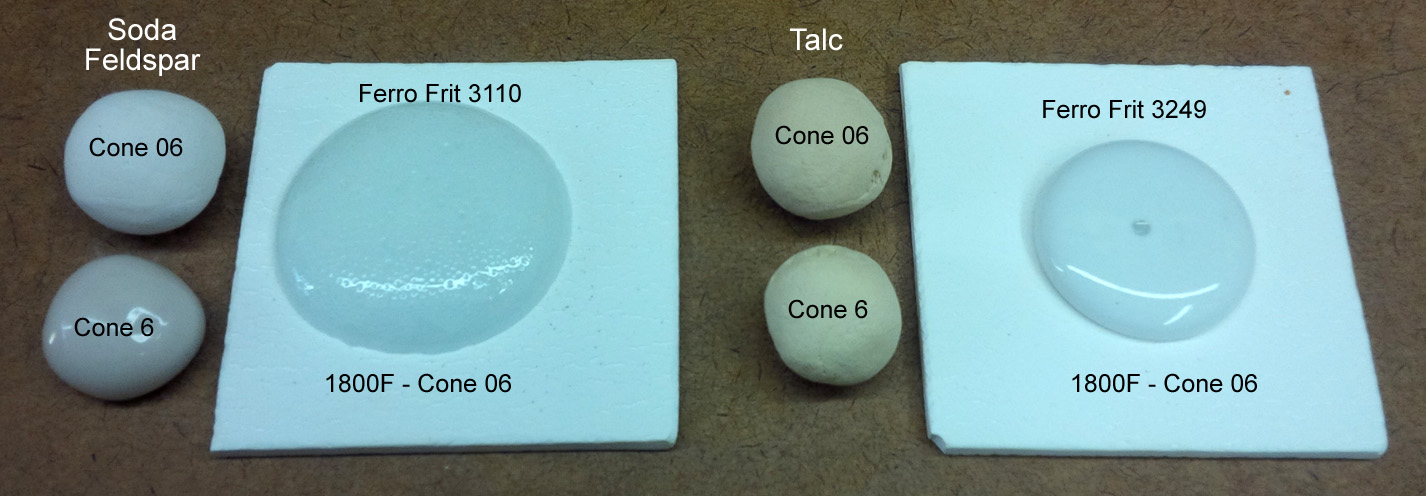
These GBMF test balls were fired at 1550F and were the same size to start. The Gerstley Borate has suddenly shrunk dramatically in the last 40 degrees (and will shrink even more and then suddenly melt down flat within the next 50). The talc is still refractory, the Ferro Frit 3124 slowly softens across a wide temperature range. The frit and Gerstley Borate are always fluxes, the talc is a flux under certain circumstances.
Frits melt so much better than raw materials
This picture has its own page with more detail, click here to see it.
Feldspar and talc are both flux sources (glaze melters), they are common in all types of stoneware glazes. But their fluxing oxides, Na2O and MgO, are locked in crystal structures that neither melt early or supply other oxides with which they like to interact. The pure feldspar is only beginning to soften at cone 6. Yet the soda frit is already very active at cone 06! As high as cone 6, talc (the best source of MgO) shows no signs of melting activity at all. But a high-MgO frit is melting beautifully at cone 06! The frits progressively soften, starting from low temperatures, both because they have been premelted and have significant boron content. In both, the Na2O and MgO are free to impose themselves as fluxes, actively participating in the softening process.
2% Copper in two cone 6 transparents:
One does not bubble and orange-peel. Why?
This picture has its own page with more detail, click here to see it.
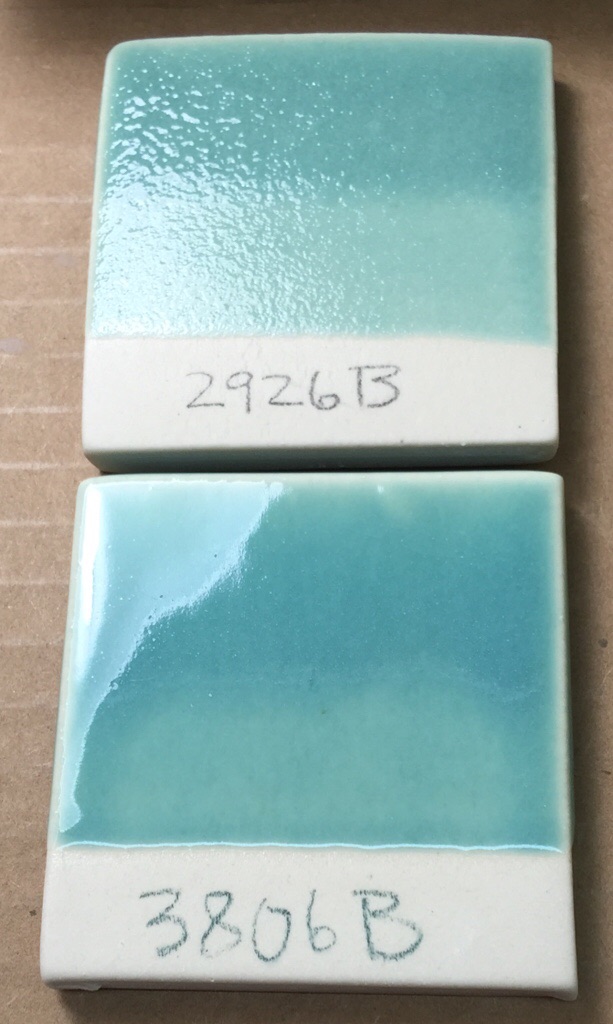
The top base glaze, G2926B, has enough melt fluidity to produce a brilliant functional gloss when used as a transparent. However, for this 2% copper carbonate addition, it has too little melt fluidity and/or too much surface tension to merge, pass and heal the entrained micro-bubbles (generated by the decomposition of the carbonate).
The lower glaze, G3806B, diversifies the fluxes (half the B2O3 in exchange for more Na2O and introduction of SrO and ZnO) and increases their total compared to Al2O3 and SiO2. The result is a more fluid cone 6 melt having lower surface tension. The mixed-oxide effect is also a factor here; the diversity itself improves the melt.
The above factors are enough to solve the problem here. But more can be done. More zinc (in exchange for KNaO) could produce later melting, especially in combination with sourcing some or all of the latter from a feldspar instead of the low-melting frit. The benefit would enable more gas escape until melt-sealing (and reduce the COE).
Pure stain powders painted overglaze:
Why the bleeding and bubbling?

This picture has its own page with more detail, click here to see it.
The blue is melting and bleeding profusely into the glaze. The green is the opposite - refractory, stiffening the glaze enough to trap bubbles and sit on the surface as a dry, unmelted layer. Under the glaze, these problems would be magnified (the blue bleeding more, the green causing crawling and blistering).
Stains are not ceramic; they are ceramic additives. Stains are not considered safe for direct food contact. Stains are expensive. Stains don't suspend in water, paint poorly and dry as a loose powder.
Both of these (and others) need to be added, as a minor percentage, to a ceramic carrier (one with CMC gum and a mix of ceramic materials tailored to melt to the desired degree and have a compatible chemistry to develop the color (as per manufacturer guidelines).
Copper fluxes a matte glaze at cone 6
This picture has its own page with more detail, click here to see it.
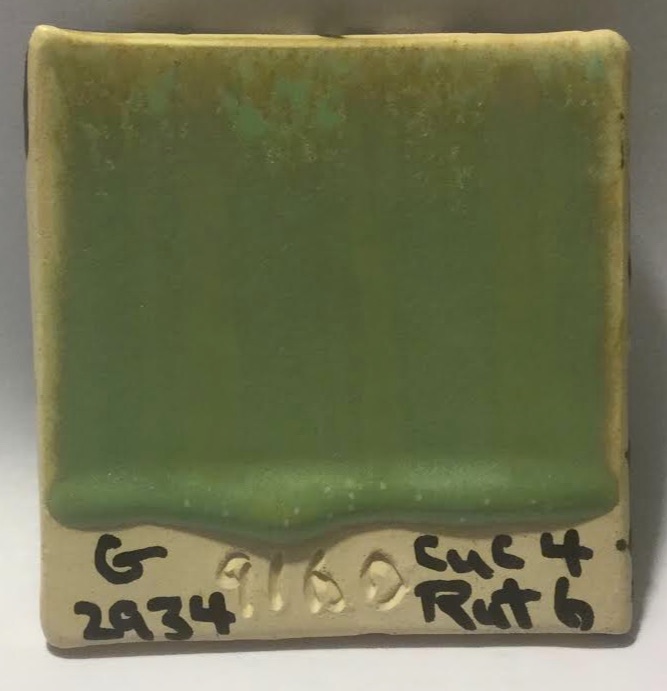
4% copper carbonate and 6% rutile have been added to G2934 cone 6 matte base. Using a green stain should prevent this. Or some B2O3 could be substituted with SiO2 (via glaze chemistry).
The amazing fluxing power of boron (in borax)

This picture has its own page with more detail, click here to see it.
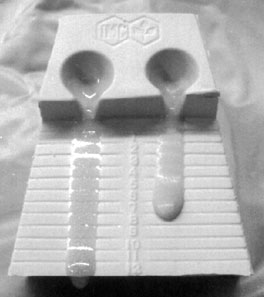
The two top clay bars contain 15% hydrous borax. At cone 06, a very low temperature, it has already melted and drained out of the bars, running down over the others as a glass.
A highly fluxed body, when over fired can do this!

This picture has its own page with more detail, click here to see it.
These two mugs are made from the same material: Ravenscrag Slip plus 20% Ferro Frit 3134. The one on the right has been bisque fired to 1550F. The one on the left has been clear glazed and fired to cone 03 (1950F). That means that this body vitrifies well below cone 03, likely well below cone 06. Thus strength, maturity, vitrification are not a matter of temperature, they are a matter of how much flux is available in the body to mature it to a dense, strong matrix.
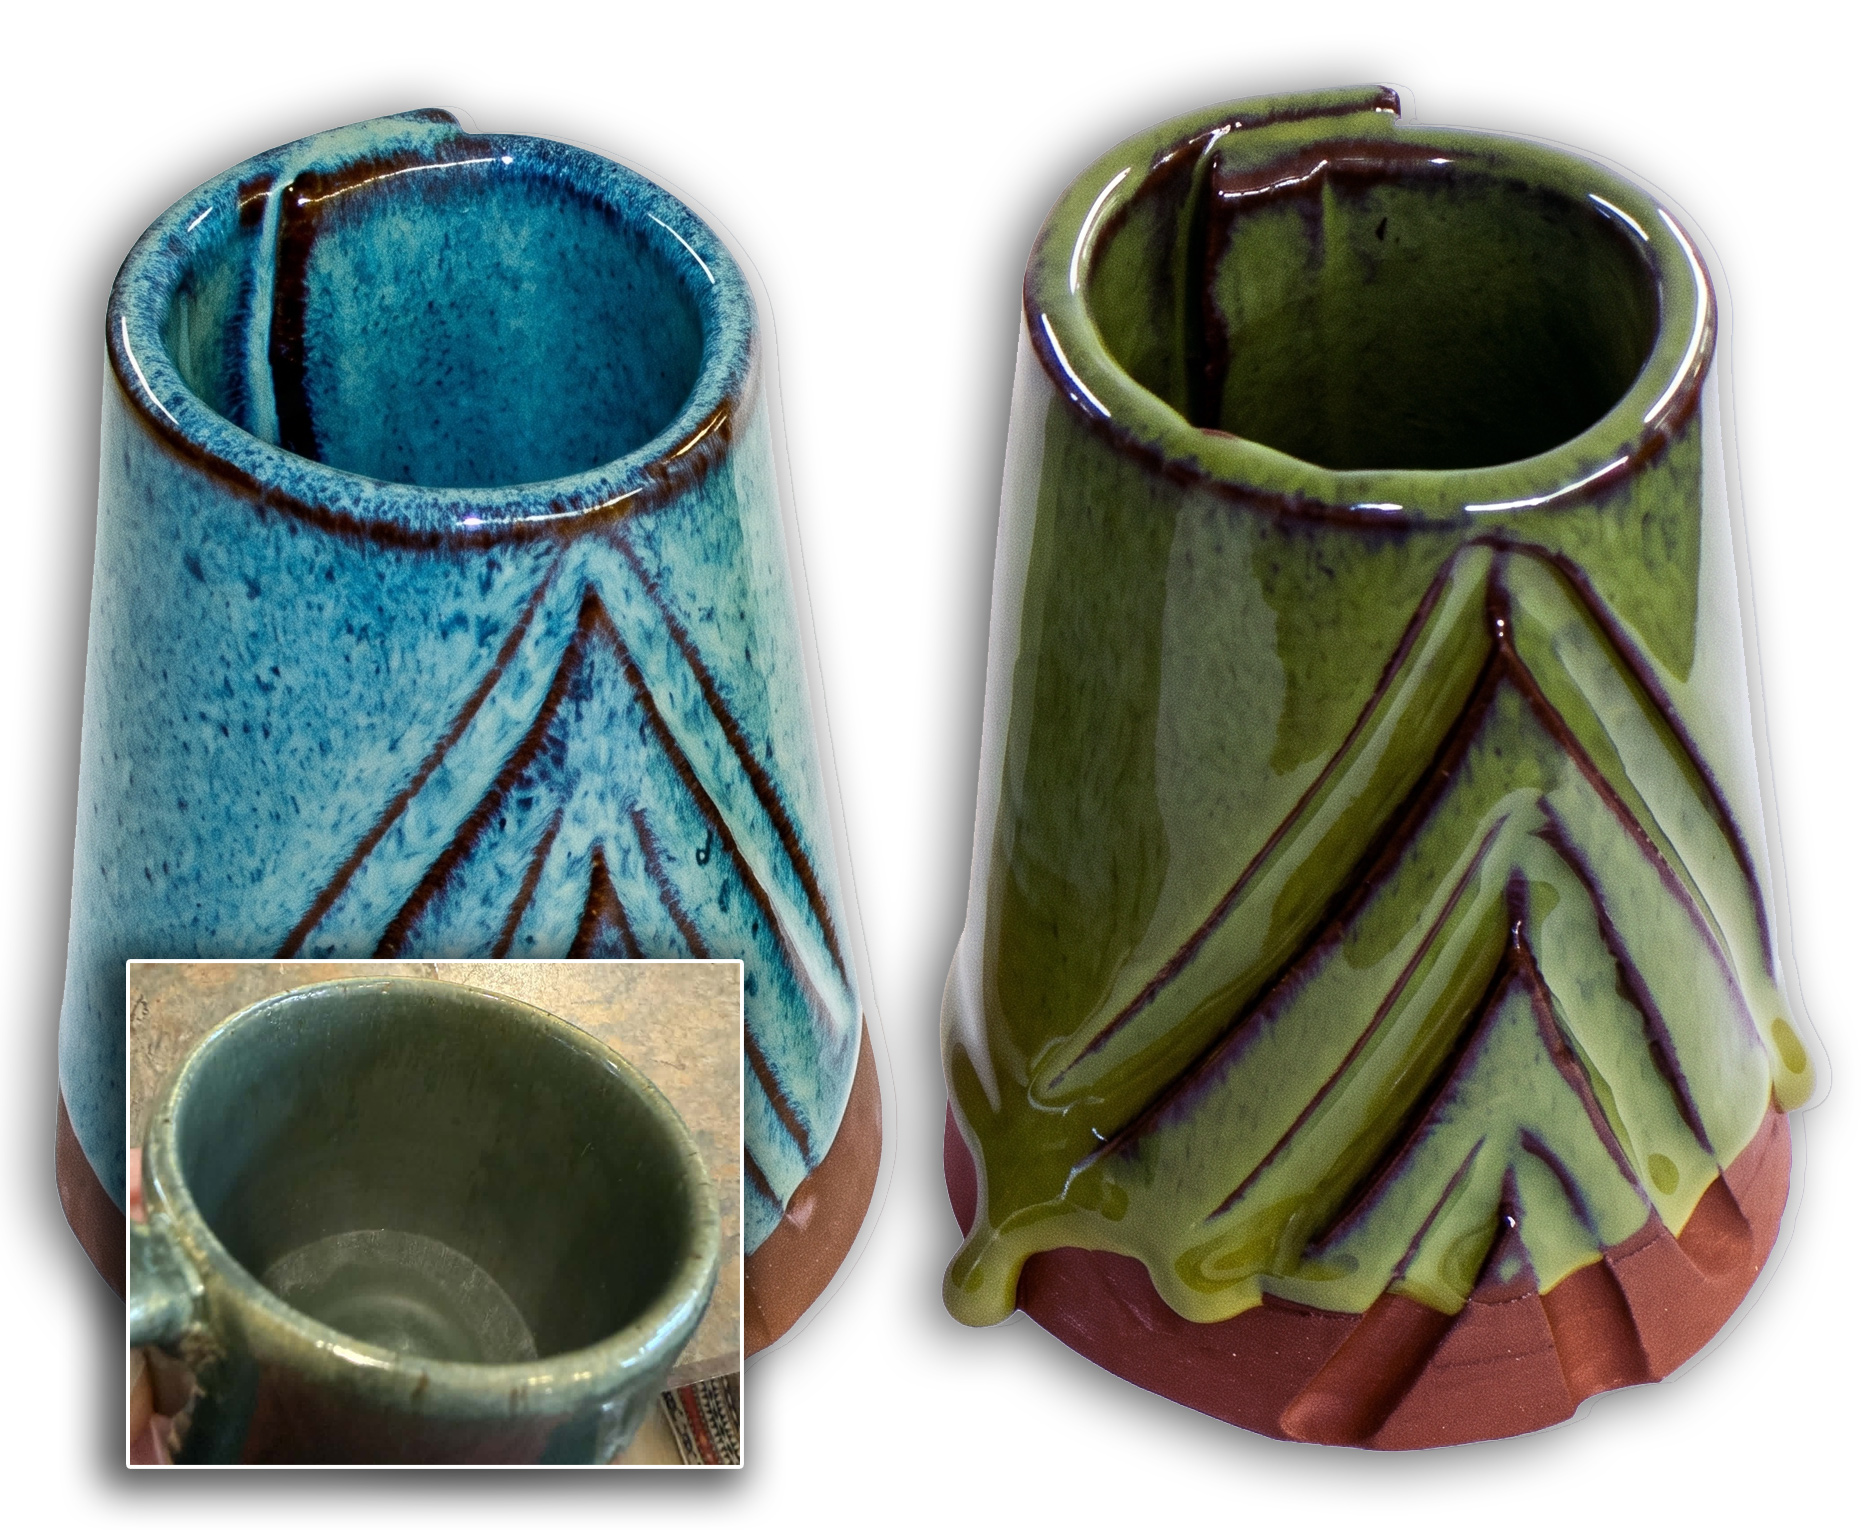
Copper is not just a pigment:
It can be a powerful flux, with consequences
This picture has its own page with more detail, click here to see it.
Left: The base recipe of GA6-C (80% Alberta Slip, 20% Frit 3134, 4% rutile). That recipe is stable; it does not run. Right: A 2% addition of copper carbonate transforms it into a runny, melt fluid glaze. It also produces a pleasant green even on this red-burning body (a good green is not easy in oxidation ceramics). Using a catch glaze (e.g. a frit-reduced version), this could be made safe on vertical surfaces. However, there are red flags here. Having only 2% copper would not destabilize a typical glaze (making it leachable). But phase separation is occurring here, likely because the base contains significant rutile. That means the phases are copper-bearing and possibly copper-concentrating. And, as noted, the copper has a greater-than-expected impact on the melt. Third, commercial variegated copper glazes can even leach in acids (as happened with the mug inset after a night with lemon juice). While the GA6-C recipe does have a 0.3:0.7 R2O:RO ratio, other indicators make it a course of wisdom to consider the GLLE test before use on functional surfaces.
Iron oxide goes crazy in reduction

This picture has its own page with more detail, click here to see it.
Cone 6 iron bodies that fire non-vitreous and burn tan or brown in oxidation can easily go dark or vitreous chocolate brown (or even melting and bloated in reduction). On the right is Plainsman M350, a body that fires light tan in oxidation, notice how it burns deep brown in reduction at the same temperature. This occurs because the iron converts to a flux and the glass development that occurs brings out the dark color. On the left is Plainsman M2, a raw high iron clay that is quite vitreous in oxidation, but in reduction it is bloating badly. When reduction bodies are this vitreous there is a much great danger of black coring.
Trying to avoid knowing anything about glaze chemistry? Be ready for drama!

This picture has its own page with more detail, click here to see it.
Maybe you don't think it is necessary to know anything about glaze chemistry to be a potter. Or a technician at a production facility. This thinking depends on how much mystery you mind tolerating. Because the reason for many of the problems you will encounter with glazes relates fundamentally to their chemistry. Perhaps you have other "social" actors in your sphere who also specialize in the "know as little technical stuff as possible" mindset. Who treat glazes like acrylic paint that comes in tubes - it is just color! From these people, you will get buying advice on expensive jars of tacky-looking "goop" that you have to laboriously paint on in layers. Or it will mean you'll be more likely to get trapped on the recipe treadmill, addicted to the traffic of recipes that never seem to work.
How can a refractory oxide be a flux?

This picture has its own page with more detail, click here to see it.
Pure calcium oxide melts at about 2570C (yet typical stoneware kilns fire around 1300C!) Yet CaO is an important flux in many stoneware glazes. How is this possible? Interactions. The contribution of CaO depends on its interaction with silica, alumina and other oxides in the melt. Thus, the melting point of the pure oxide does not predict the melting temperature of a mixture containing it.
The test tiles show 2%, 5%, 10% and 15% calcium carbonate additions to Ravenscrag Slip on a buff stoneware fired at cone 10R (prepared by Kat Valenzuela). Notice the glaze gets progressively glossier toward 15% (crazing also starts at 10%).
Inbound Photo Links
 Stains having varying fluxing effects on a host glaze |
Links
| Typecodes |
Flux Source
Materials that source Na2O, K2O, Li2O, CaO, MgO and other fluxes but are not feldspars or frits. Remember that materials can be flux sources but also perform many other roles. For example, talc is a flux in high temperature glazes, but a matting agent in low temperatures ones. It can also be a flux, a filler and an expansion increaser in bodies. |
| Glossary |
Refractory
In the ceramic industry, refractory materials are those that can withstand a high temperature without deforming or melting. Or can be sintered into super materials. |
| Glossary |
Frit
Frits are used in ceramic glazes for a wide range of reasons. They are man-made glass powders of controlled chemistry with many advantages over raw materials. |
| Glossary |
Limit Formula
A way of establishing guideline for each oxide in the chemistry for different ceramic glaze types. Understanding the roles of each oxide and the limits of this approach are a key to effectively using these guidelines. |
| Oxides | CaO - Calcium Oxide, Calcia |
| Oxides | K2O - Potassium Oxide |
| Oxides | Li2O - Lithium Oxide, Lithia |
| Oxides | Na2O - Sodium Oxide, Soda |
| Oxides | MgO - Magnesium Oxide, Magnesia |
| Oxides | SrO - Strontium Oxide, Strontia |
| Oxides | BaO - Barium Oxide, Baria |
| Oxides | B2O3 - Boric Oxide |
| Oxides | ZnO - Zinc Oxide |
| Troubles |
Runny Ceramic Glazes
Glazes of high melt fluidity are likely to run if applied to thickly or have not catcher glaze |
| Articles |
What Determines a Glaze's Firing Temperature?
The oxides contributed by glaze materials determine its chemistry. The chemistry is the main factor determining melting behaviour. But the particle sizes, shapes and mineralogies also come in to play. |
 PayPal | No tracking, No ads, No paywall, No transient content! Just organized, concise information constantly updated and improved. Was this helpful? Consider supporting me. |
| By Tony Hansen Follow me on        |  |
Got a Question?
Buy me a coffee and we can talk 

https://digitalfire.com, All Rights Reserved
Privacy Policy