Casting Rate
Casting rate describes how quickly a layer of clay builds against the mold surface during slip casting and how quickly items release from molds and can be handled.
Key phrases linking here: casting rate - Learn more
Details
Casting rate describes how quickly a layer of clay builds against the mold surface during slip casting. In conventional plaster molds, capillary suction draws water from the slip, leaving a consolidated layer of particles behind. Water must then pass through this layer for more material to deposit. As the wall thickens, resistance to water movement increases, and further buildup slows. Thus, twice the casting time does not produce twice the wall thickness. For practical comparisons, casting rate can be assessed by measuring the thickness produced in a fixed time or the time needed to reach a specified thickness.
Casting rate depends strongly on the permeability of the deposited layer. While influenced by particle size distribution, particle packing and the degree of deflocculation, the main factor is the nature of the clays used, especially their plasticity. Very fine plastic clays can provide excellent strength but form layers through which water moves slowly. Larger-particle clays, which are less plastic, can build thickness much faster. However, speed alone is not the objective: The cast must also develop enough strength and drying shrinkage to pull itself away from the mold as it shrinks. The formulation challenge is to obtain sufficient strength and reliable release while retaining good permeability.
Mold release can also be affected by the stickiness of the clays used. Some kaolins are very sticky even though not highly plastic, this can affect how cleanly pieces release from the mold. It is well worth the effort to compare candidate kaolins in the intended body recipe, developing a mix of them that gives the best performance.
Casting rate is also a property of the slip-and-mold combination, not simply of the body recipe. Just as wet molds cast more slowly, lots of intricate surface detail affects casting time (or even the ability to pull a successful piece at all). It may be that you need a different casting slip recipe for certain types of molds, accepting a slower casting rate in them for better release and retention of surface detail.
A testing program is important to streamline production. Record things like wall-building time, release failures and why, release time and characteristics, surface quality and handling strength (all under consistent slip and mold conditions). The practical objective is a short, reliable cycle that produces sound ware for each type of mold.
Related Information
Demonstrate casting-rate control:
By slip-casting nepheline syenite

This picture has its own page with more detail, click here to see it.
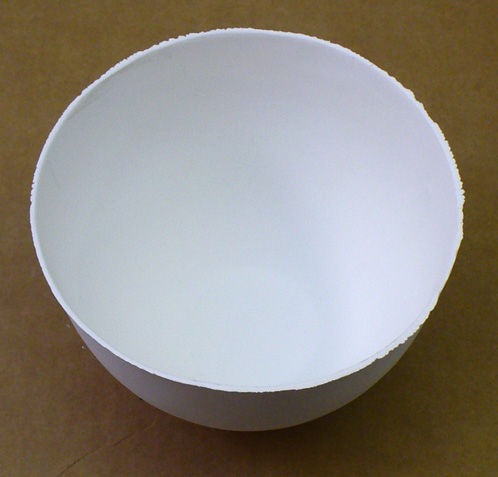
What would it take to cast pure Nepheline Syenite? A clay addition. This 10:90 bentonite:Nepheline has enough shrinkage and leather-hard strength to enable pulling itself away from the plaster mold. This bowl was just extracted; it cast without cracks to 3mm thickness in about 15 minutes. The defloculated slip required more water than normal but it pours and drains really well. This is a demonstration of how much control technicians can have over casting rate. The amount and type of plastic clay added can take this material from being completely water permeable, zero leather-hard strength and non-castable to water impermeable, very high leather-hardness but very slow casting. Only a testing program is needed to determine the minimum bentonite percentage needed to achieve reliable casting (it is likely less than 10%).
For example, 95%+ nepheline slurries can be made using Veegum. How did this bowl fire? As a vitreous product around cone 1. And, on aging for a month, the rheological properties of the slurry did not change.
NZ kaolin-based slip casts at 1mm thickness. How?
This picture has its own page with more detail, click here to see it.
This is Polar Ice casting, a cone 6 translucent porcelain that uses New Zealand Halloysite. The base body recipe would never have enough plastic strength to pull itself from this mold without tearing. But the addition of 1% Veegum gives it amazing strength. This dried cast bowl measures 130mm in diameter and 85mm deep; it only weighs 89 gm! The slip was in the mold for only 1 minute before pour-out. Of course, there is a price to pay for adding the Veegum: Increased casting time and more difficult deflocculation. This 1% addition can be refined. A program of testing could indicate that a lower percentage of Veegum could work, increasing the casting rate. The polar ice information page has very good information, under the heading “Casting Recipe” (it deals with the trade-offs of using this kaolin in casting bodies).
This cone 6 porcelain casts super-fast
The type of kaolin and ball clay is the secret

This picture has its own page with more detail, click here to see it.
Rather than L4807 being just another cone 6 porcelain casting slip recipe it is a pattern of the flexibility potters/hobbyists could have in making their own bodies. This has incredible casting speed. If someone tells you that porcelains are always difficult to cast, tell them it’s time to go DIY.
Typical slips made from ball clay and talc (or mixes of common feldspars, clays and quartz) take 20-30 minutes to get the needed thickness (in our circumstances and assuming a new dry mold). But this one poured out in 12 minutes and I can demold in 10 minutes. The secret is not the recipe, this is similar to a typical 25-porcelain. The secret here is choice of kaolin and ball clay. This employs OptiKast Kaolin and KT#1-4 ball clay, both are large particled clays targeted at slip casting. They can be traded off for each other, more ball clay imparts better leather-hard strength but casts slower, more kaolin does the opposite. This is one more reason to mix your own casting bodies.
Kaolin and ball clay:
Why the uncracked disk is not the whole story
This picture has its own page with more detail, click here to see it.
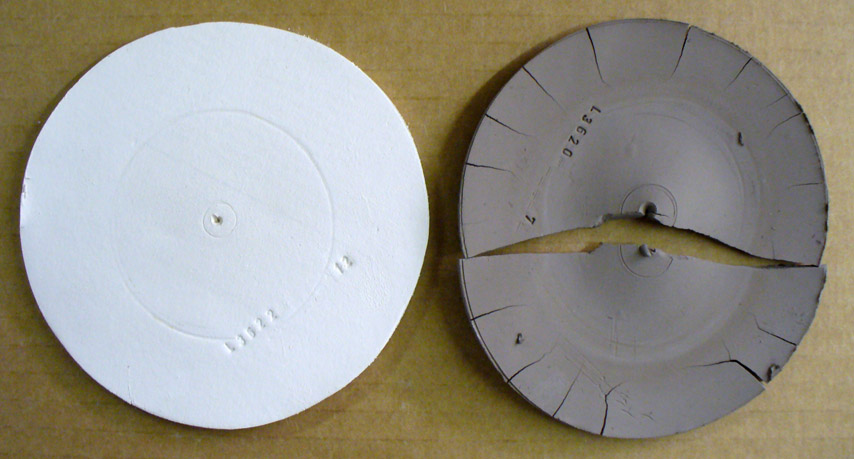
Left: OptiKast, a coarse-particle kaolin intended for slip-casting. Right: Plainsman A2 ball clay. These DFAC test (drying performance) disks were dried with their centers covered, deliberately creating uneven drying. The exposed perimeter dries and stiffens first; the covered center dries and shrinks later. The resulting cracks reveal how each clay responds to that stress. OptiKast feels smoother, yet its individual clay particles are much coarser than those typical of ball clay. This kaolin has low drying shrinkage, so its disk remained intact. The ball clay shrinks more. As its center dried and tried to contract against the already stiff perimeter, stresses developed, splitting the disk and opening numerous cracks around the edge.
So why use ball clay? This particular kaolin has so little plasticity that even making this disk was difficult. And the dried disk is fragile. Yet it is very useful in casting bodies, where plasticity impedes permeability. Ball clays are highly plastic; high drying shrinkage comes with that. Adding some of this to poor-plasticity casting or forming bodies that can tolerate a darker fired color can transform them into ones that both form well and dry harder and stronger.
Links
| Glossary |
Slip Casting
A method of forming ceramics. A deflocculated (low water content) slurry is poured into absorbent plaster molds. As it sits in the mold, usually 10+ minutes, a layer builds against the mold walls. When thick enough the mold is drained. |
 PayPal | No tracking, No ads, No paywall, No transient content! Just organized, concise information constantly updated and improved. Was this helpful? Consider supporting me. |
| By Tony Hansen Follow me on        |  |
Got a Question?
Buy me a coffee and we can talk 
https://digitalfire.com, All Rights Reserved
Privacy Policy