OptiKast Kaolin
Alternate Names: OptiCast
Description: Large Particle Size Kaolin
| Oxide | Analysis | Formula | Tolerance |
|---|---|---|---|
| SiO2 | 45.20% | 1.98 | |
| Al2O3 | 38.70% | 1.00 | |
| Fe2O3 | 0.50% | 0.01 | |
| TiO2 | 1.60% | 0.05 | |
| CaO | 0.10% | - | |
| K2O | 0.10% | - | |
| Na2O | 0.10% | - | |
| LOI | 13.60% | n/a | |
| C | 0.03% | n/a | |
| SO3 | 0.04% | n/a | |
| Oxide Weight | 227.46 | ||
| Formula Weight | 263.47 | ||
Notes
optiKast is a coarse-grained kaolin used primarily in ceramic casting applications. It has a very fast cast and exceptional deflocculation characteristics. Thus optiKasT is preferred in pressure casting systems.
Velvacast kaolin is no longer available, this is the recommended substitute. One concern with Velvacast was its dark fired color (compared to other common plastic kaolins). Opticast has higher iron and TiO2 contents, this will impact whiteness and certainly translucency in porcelains. We have done fired shrinkage, porosity, dry performance and plasticity comparison tests between these two materials Oct 2011 and they do appear very similar, Opticast is a little more plastic than Velvacast and does not appear to fire darker at cone 8 and 10.
Related Information
This cone 6 porcelain casts super-fast
The type of kaolin and ball clay is the secret

This picture has its own page with more detail, click here to see it.
Rather than L4807 being just another cone 6 porcelain casting slip recipe it is a pattern of the flexibility potters/hobbyists could have in making their own bodies. This has incredible casting speed. If someone tells you that porcelains are always difficult to cast, tell them it’s time to go DIY.
Typical slips made from ball clay and talc (or mixes of common feldspars, clays and quartz) take 20-30 minutes to get the needed thickness (in our circumstances and assuming a new dry mold). But this one poured out in 12 minutes and I can demold in 10 minutes. The secret is not the recipe, this is similar to a typical 25-porcelain. The secret here is choice of kaolin and ball clay. This employs OptiKast Kaolin and KT#1-4 ball clay, both are large particled clays targeted at slip casting. They can be traded off for each other, more ball clay imparts better leather-hard strength but casts slower, more kaolin does the opposite. This is one more reason to mix your own casting bodies.
Kaolin and ball clay:
Why the uncracked disk is not the whole story
This picture has its own page with more detail, click here to see it.
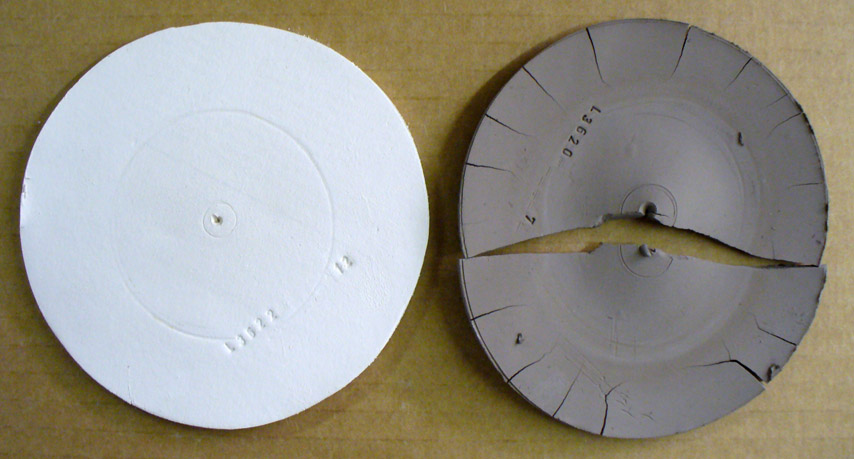
Left: OptiKast, a coarse-particle kaolin intended for slip-casting. Right: Plainsman A2 ball clay. These DFAC test (drying performance) disks were dried with their centers covered, deliberately creating uneven drying. The exposed perimeter dries and stiffens first; the covered center dries and shrinks later. The resulting cracks reveal how each clay responds to that stress. OptiKast feels smoother, yet its individual clay particles are much coarser than those typical of ball clay. This kaolin has low drying shrinkage, so its disk remained intact. The ball clay shrinks more. As its center dried and tried to contract against the already stiff perimeter, stresses developed, splitting the disk and opening numerous cracks around the edge.
So why use ball clay? This particular kaolin has so little plasticity that even making this disk was difficult. And the dried disk is fragile. Yet it is very useful in casting bodies, where plasticity impedes permeability. Ball clays are highly plastic; high drying shrinkage comes with that. Adding some of this to poor-plasticity casting or forming bodies that can tolerate a darker fired color can transform them into ones that both form well and dry harder and stronger.
First Mug From v1 Prototype Mold

This picture has its own page with more detail, click here to see it.
This plaster test mold is thin-walled yet I can cast three thick-walled mugs in three hours. This clay is L2596G, a buff burning cone 10 stoneware - the mug on the lower right has been fired to cone 10 oxidation. Achieving 4-5mm thick walls is not a problem if the casting slip employs a large particle kaolin intended for this purpose (e.g. OptiKast). And it is deflocculated properly.
The flared lip works as expected, keeping the rim nice and round. No cracks have appeared at handle joins, even for pieces left in the mold overnight. The mold halves mate with each other very well and the seam is easy to remove. The seam on the base is an issue - I have to be careful to line up the halves well before clamping the mold strap - this is a warning for accuracy during the mold production stage. And the possible motive for a three-piece mold if I get more serious about this piece.
Links
| Typecodes |
Kaolin
Pure clay mineral, there are many brand names of varying purity and iron content. |
| Materials |
Velvacast Kaolin
|
Data
| % < 0.5 microns | 18.0 |
|---|---|
| % < 5 microns | 74.0 |
| % Passing 325 Mesh Wet | 94.0 |
| Modulus of Rupture - Dry | 225 psi (50/50 clay/silica) |
| Surface Area (m2/gm) | 11.0 |
| % < 20 microns | 94.0 |
| % < 10 microns | 85.0 |
| % < 2 microns | 55.0 |
| % < 1 micron | 37.0 |
| pH for dry powder | 5.7 |
 PayPal | No tracking, No ads, No paywall, No transient content! Just organized, concise information constantly updated and improved. Was this helpful? Consider supporting me. |
| By Tony Hansen Follow me on        |  |
Got a Question?
Buy me a coffee and we can talk 
https://digitalfire.com, All Rights Reserved
Privacy Policy